👋 Welcome to Reflex Industrial Solutions
Empowering Industries with Reliable Chemical Solutions
We are Reflex Industrial Solutions. An elite water management agency that caters to the water related problems of all types and diversity. The company offers water management solutions to entire gamut of industries.
Engineered Water & ChemicalOperational Capabilities
Surveys, analysis, and system reviews for efficiency, pretreatment systems, ongoing support, and waste management.
Water and Energy Audits
Surveys, analysis, and system reviews for efficiency.
Pretreatment Systems
Supply, setup, and upkeep of filters, RO, and softeners.
Support and Maintenance
AMCs, operator training, and technical services.
Chemical and Waste Management
Metal treatment and sludge management solutions.
Engineering Reliable Water Solutions for Heavy Industry
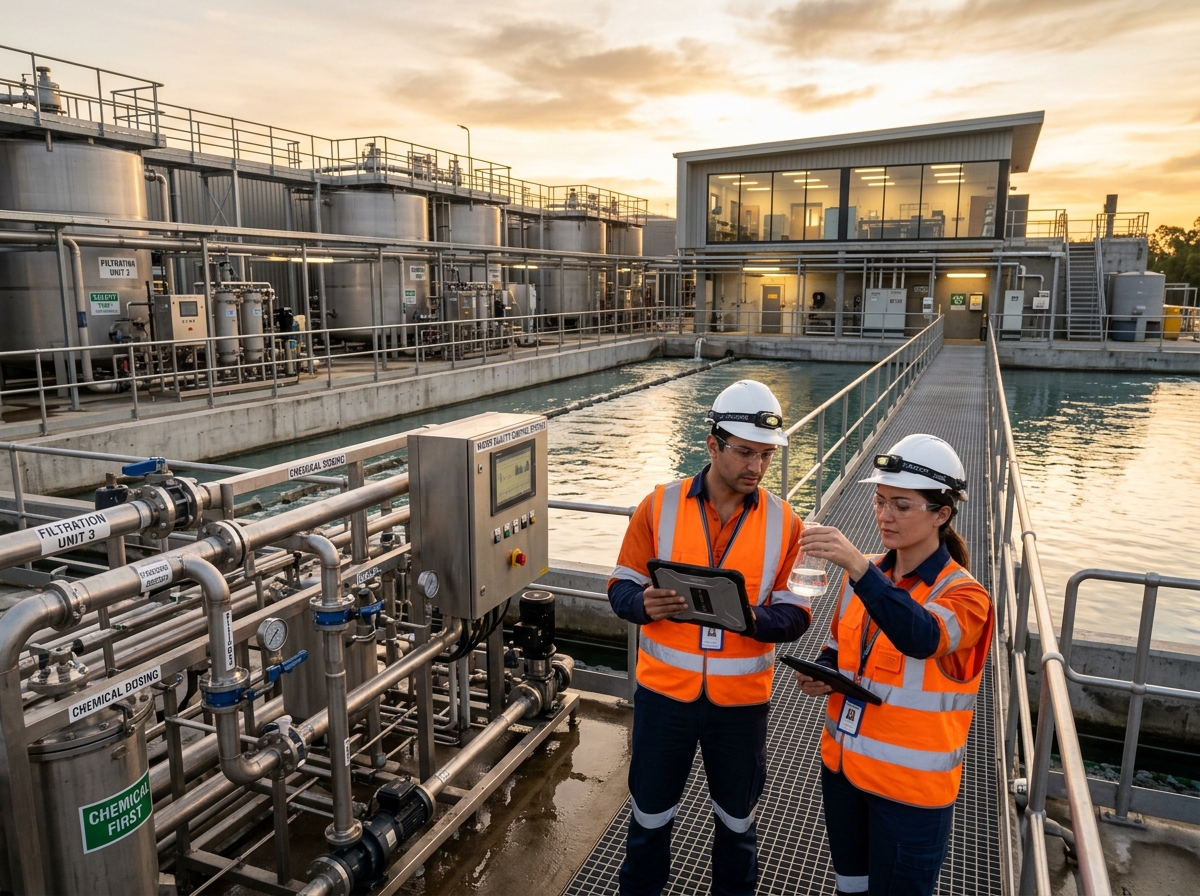
We are Reflex Industrial Solutions. An elite water management and industrial chemical solutions agency that caters to water-related engineering challenges of all types and diversity. The company offers advanced water management solutions to the entire gamut of industries such as fertilizer, petroleum refining, petrochemicals, power generation, mining, and mineral processing.
High-Performance Chemical Formulations& Industrial Treatment Systems
Engineered specifically for heavy industrial utilities, our high-purity chemical blends and automated monitoring technologies protect vital assets, maximize thermal efficiency, and guarantee environmental compliance.
Boiler Water Treatment
Corrosion & Scale Inhibition
High-performance oxygen scavengers, polymer conditioners, and alkalinity builders formulated for low to ultra-high pressure steam boilers.
Fuel & Fireside Treatment
Combustion Optimization
Solid fuel additives and furnace oil conditioning catalysts that elevate thermal heat transfer while mitigating slagging and acid dew point corrosion.
Cooling Water Treatment
Heat Exchanger Defense
Broad-spectrum oxidizing & non-oxidizing biocides, biodispersants, and organic corrosion inhibitors for open recirculating and closed loops.
Raw & Wastewater Treatment
Zero Discharge Clarification
Specialized coagulants, polyamines, heavy metal precipitants, and high-molecular flocculants engineered for zero liquid discharge (ZLD).
Reverse Osmosis / UF / Nano
Membrane Life Extension
NSF-certified membrane antiscalants, precision silica dispersants, and CIP chemical cleaners that restore flux and extend membrane longevity.
Speciality Products
Tailored Process Chemistries
Custom specialty formulations for sugar processing, refineries, paint booths, metal finishing, and customized industrial descaling.
Plants & Monitoring Equipment
Telemetry & Automated Skids
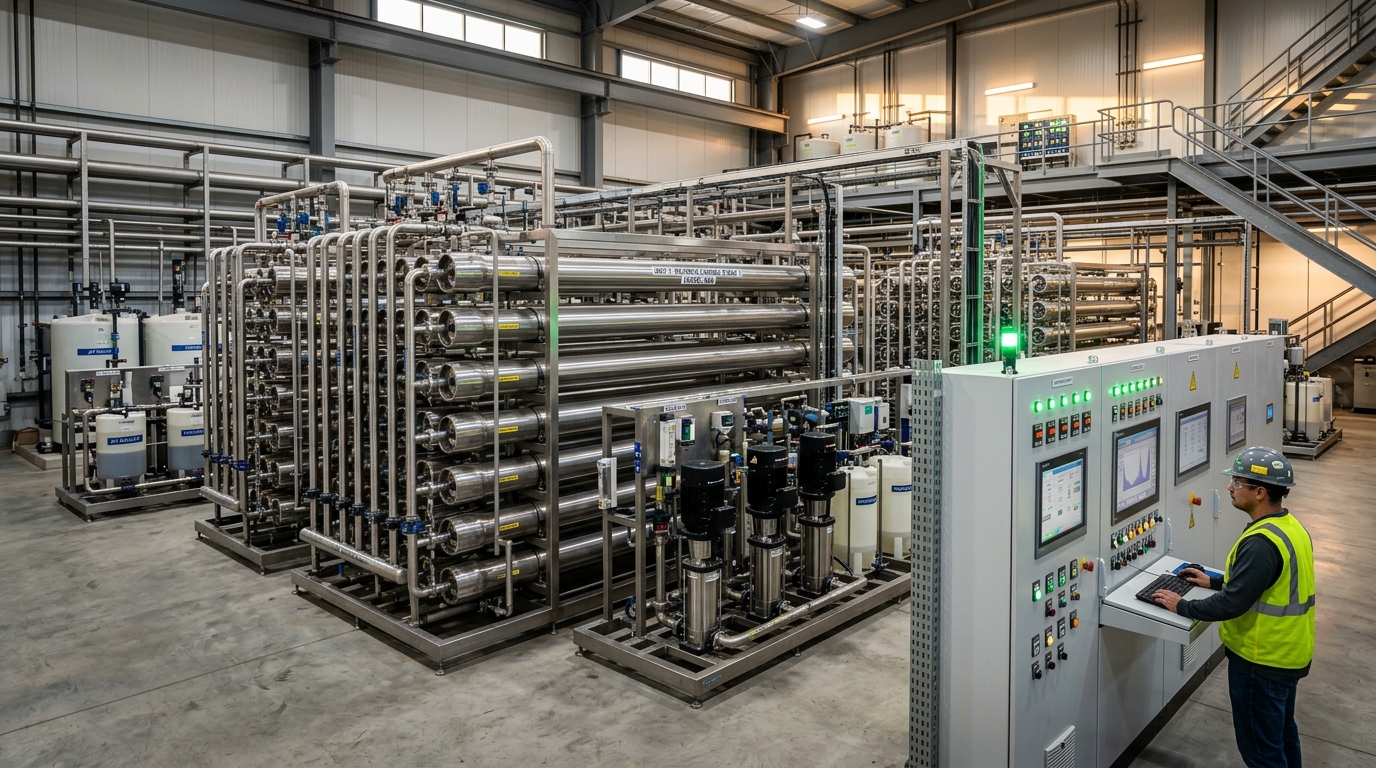
Smart automated chemical dosing skids, inline pH/ORP controllers, conductivity monitors, and digital real-time water quality telemetry.
Boiler Feed Water Treatment
Demineralization & Polishing
Ion exchange resin regeneration chemicals, condensate return line neutralizing amines, and feed-water de-aerator protective chemistries.
Industrial Engineering Services& Utility Management Solutions
From comprehensive thermodynamic water and energy audits to turnkey plant commissioning, critical spares supply, and continuous certified laboratory scale analysis.
Speak with a Senior Water Engineer
Quality Policy
It is absolutely essential to ensure that the goods produced are of the right quality to ensure trouble-free operation at site. It is also essential that the inputs used meet stringent quality requirements, which is a prerequisite for meeting the finished product specifications. To fulfill this important requirement, Reflex Industrial Solutions has a well laid out process :
Goods not meeting our specification are rejected and not used.
Raw materials that have minor deviations are used only with the proper approvals.
Production manufactures the products strictly as per the procedure laid down in the Production Manual.
Finished product is analyzed in totality as per the specifications laid down in the Finished Products manual.
Only products that meet the specifications in all respects are cleared for further dispatch.
A sample from every batch that has been cleared for dispatch is retained for future reference and complaints, if any.
Random sampling of packed batches and their analysis are conducted periodically.
Every consignment is accompanied with a Certificate of Quality.