Quality Policy & Analytical Assurance
It is absolutely essential to ensure that the goods produced are of the right quality to guarantee trouble-free operation at site. It is also essential that the inputs used meet stringent quality requirements, which is a prerequisite for meeting the finished product specifications. To fulfill this critical requirement, Reflex Industrial Solutions operates an uncompromising, multi-tiered quality management system spanning raw material qualification, formulation discipline, analytical testing, and outbound certification.
100%
Mandatory raw material verification & COA validation
Zero-Defect
Immediate quarantine of any non-compliant component
Archived
Retained reference sample from every cleared batch
COA Mandatory
Certificate of Quality issued with every consignment
The 4-Stage Quality Gate Lifecycle
Inward Raw Material Verification
Every single incoming raw material must satisfy strictly laid-down physical and chemical specifications before entering our production chain.
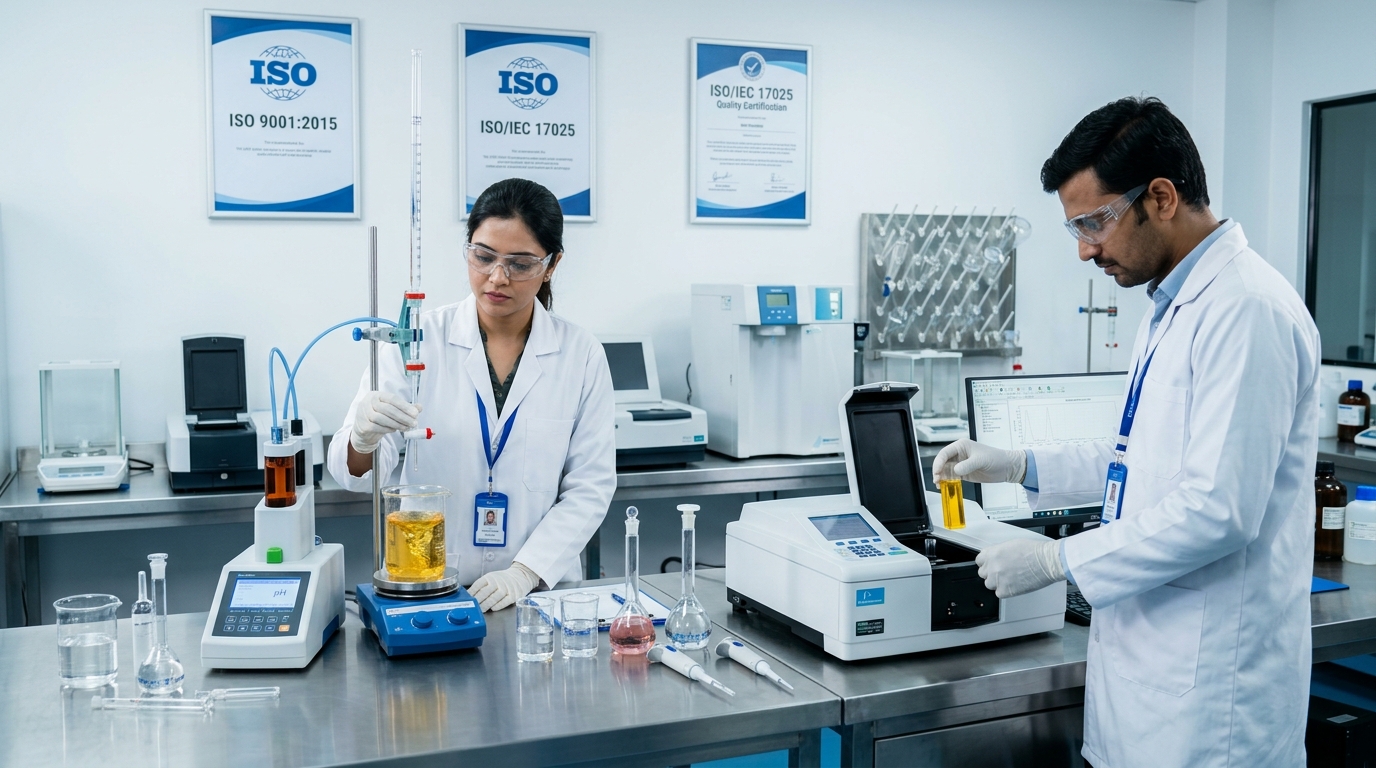
ISO 9001:2015 Accredited Quality Standards
The 11 Master Quality Directives
Laid Down Specifications
Every raw material purchased has strictly laid down physical and chemical specifications.
Mandatory Vendor Certificates
Vendors must provide an authentic quality certificate with each of their consignments.
Certified Vendor Preference
Vendors that consistently provide verified quality certificates are actively preferred.
Zero-Defect Inflow Rejection
Goods and chemical inputs not meeting our specifications are strictly rejected and never used.
Controlled Deviation Protocol
Raw materials that exhibit minor deviations are used only with formal, multi-sign-off engineering approvals.
Production Manual SOPs
Production manufactures the products strictly as per the procedures laid down in the official Production Manual.
Total Product Analytics
Every finished product is analyzed in totality as per the specifications laid down in the Finished Products manual.
Unconditional Dispatch Authorization
Only products that meet specifications in all respects without exception are cleared for further dispatch.
Retained Reference Sample Archive
A sample from every batch cleared for dispatch is systematically retained for future reference, investigations, and technical audits.
Periodic Warehouse Sampling
Random sampling of packed inventory batches and comprehensive re-analysis are conducted periodically in our storage facilities.
Mandatory Certificate of Quality
Every outbound consignment is accompanied by an official, authenticated Certificate of Quality (COA).
Certified Analytical Testing Parameters
| Analytical Parameter | Testing Methodology & Standard | Engineering Purpose & Site Benefit |
|---|---|---|
Active Polymer & Solids % | Oven Desiccation & Gravimetric Analysis | Ensures precise chemical concentration for antiscalants and dispersants. |
pH & Electrolytic Conductivity | Digital Temperature-Compensated Probes | Validates solution balance and ionic integrity across operating temperatures. |
Specific Gravity & Density | Hydrometric Pycnometry @ 25°C | Confirms batch uniformity and accurate volumetric dosing skids. |
Viscosity & Rheology | Rotational Brookfield Viscometry | Ensures smooth pumping through industrial chemical dosing pumps. |
Inhibitor Efficacy & Corrosion Rate | Electrochemical Linear Polarization Resistance | Verifies metallurgical protection against corrosion in cooling and boiler loops. |
Phase Stability & Flash Point | Thermal Cycling & Closed Cup Tester | Guarantees safe transportation, bulk storage, and operational stability. |